Quick answer: A forged-roll RFQ should define the barrel, necks, transitions, service duty, material standard, hardness locations, heat treatment, machining or grinding stock, UT coverage and certificate package. One hardness number is not a complete specification.
What the buyer is really deciding
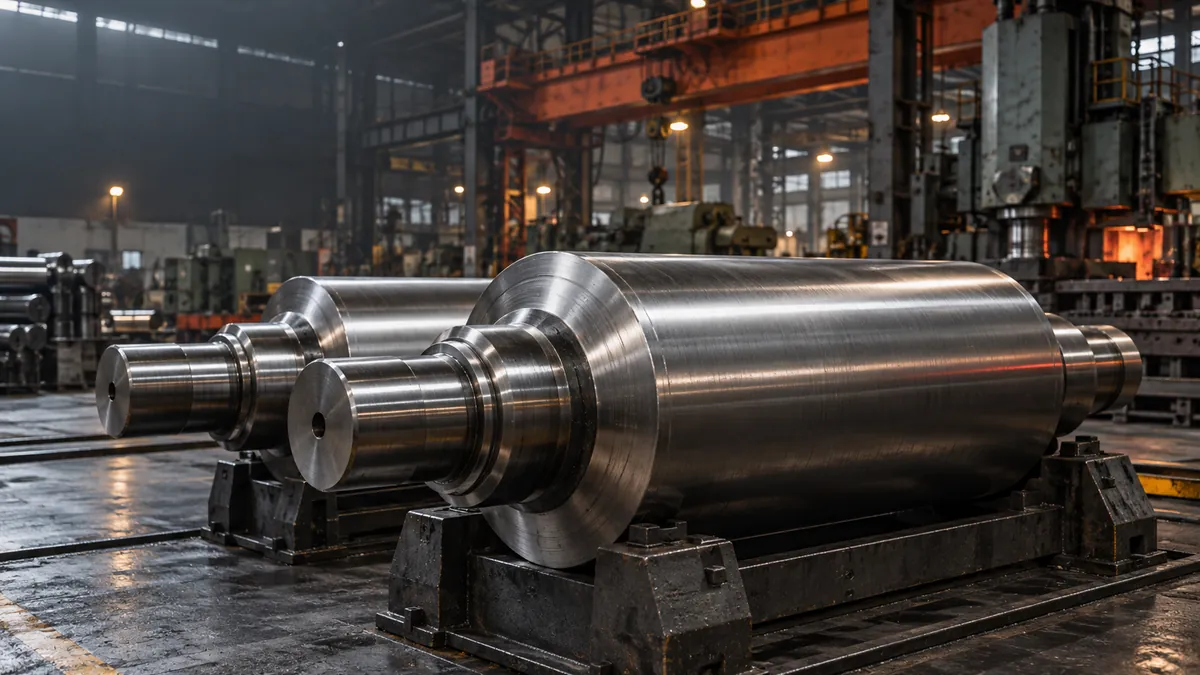
Rolling-mill rolls combine load, wear, thermal and surface requirements. Buyers should connect each acceptance criterion to a location and stage so the supplier can plan forging, heat treatment and machining without guessing.
The decision should remain evidence-led. CS Heavy Forgings has not used fabricated customer results, rankings or anonymous testimonials in this guide. Instead, the recommendations focus on documents and acceptance points that a purchasing or engineering team can verify for its own requirement.
Information to resolve before requesting price
- Barrel diameter, face length and total roll length.
- Neck diameters, keyways, drive features and transition radii.
- Mill type, stand position and expected service conditions.
- Material grade and governing standard.
- Surface and core hardness ranges with test positions.
- Rough-machined or finish-ground delivery condition.
- UT standard, zones, acceptance class and reporting.
- Balance, runout, surface finish and dimensional records.
Not every item will apply to every component, but leaving a critical item open usually forces the supplier to make an assumption. Ask each bidder to list assumptions beside the quotation so technical and commercial comparisons remain fair.
| Review area | Buyer should provide | Expected supplier response |
|---|---|---|
| Barrel | Diameter, face and wear duty | Forging envelope and hardness plan |
| Necks | Geometry, drive features and transitions | Machining datums and stress control |
| Material | Grade, heat treatment and hardness map | Defined test points and tolerances |
| Acceptance | UT, dimensions, runout and finish | Complete inspection record |
How to use this guide without over-specifying the process
The buyer should define service requirements, mandatory standards and acceptance evidence while allowing a qualified manufacturer to propose a practical production route. If a route is mandatory for design or regulatory reasons, state it explicitly. Otherwise, request a written route proposal and send deviations back to the responsible engineer for approval.
Online guidance cannot replace design validation. Dimensions, grade equivalence, heat treatment, property targets and inspection levels must be confirmed for the real component. This is especially important when a familiar grade name is used across standards or when section size changes the expected heat-treatment response.
Forged Rolls for Rolling Mills: Specification and RFQ Checklist is an engineering and purchasing question, not simply a phrase to add to a quotation. A reliable answer connects the drawing, material specification, manufacturing route, heat treatment, inspection plan and final supply condition. This guide explains the decisions an industrial buyer should document before asking a forging supplier to confirm feasibility.
CS Heavy Forgings operates from Mandi Gobindgarh, Punjab, India. The company reviews custom requirements for heavy industrial components against the submitted drawing and specification. Published ranges and examples are useful for initial screening, but final capability must always be confirmed for the actual grade, geometry, weight, quantity and test plan.
Quick answer: Forged rolls for rolling mills should be evaluated through the complete manufacturing and inspection route. Buyers should avoid approving a source from a grade name, finished weight or price alone.
Why this topic matters to industrial buyers
The practical purpose of forged roll design, hardness planning and rolling-mill service requirements is to reduce technical uncertainty before production begins. An incomplete enquiry can produce quotations that appear comparable but include different assumptions about stock, heat treatment, machining, testing or certification. Those differences often become visible only after an order is placed.
A technically complete enquiry gives the manufacturer enough information to select starting material, plan deformation, define intermediate dimensions, reserve machining allowance and place tests at meaningful stages. It also gives the buyer a clear basis for comparing suppliers and reviewing any proposed deviation.
No article can approve a component for service. The responsible designer or purchasing authority must confirm the governing standard, design loads, acceptance criteria and legal or customer-specific requirements.
Technical factors to define before quotation
- Barrel diameter, face length, neck geometry and total weight.
- Roll duty, contact pressure, thermal cycling and wear pattern.
- Material grade, hardenability and heat-treatment route.
- Surface and core hardness targets with measurement locations.
- Machining condition, grinding stock and surface-finish responsibility.
- Ultrasonic inspection, dimensional reporting and traceability.
These factors should be read together. For example, a grade that performs well in a modest section may require a different heat-treatment strategy in a much larger section. Likewise, an inspection requirement is meaningful only when the method, examination stage, coverage and acceptance class are stated.
A practical five-step evaluation sequence
1. Freeze the design inputs
Issue a controlled finished-component drawing and, where available, a forging drawing. Identify revision status, dimensions, tolerances, machining datums and any surfaces that must remain free from repair or decarburization. If the supplier is expected to develop the forging envelope, state that responsibility clearly.
2. Define material and heat treatment
Use the complete material standard and edition rather than a shortened grade name. State the delivery condition, required mechanical properties, hardness range and any impact-temperature requirement. Approximate international equivalents should not be substituted without written approval.
3. Match inspection to component risk
Choose chemical, mechanical, hardness, dimensional and non-destructive tests according to the failure risk and purchase specification. State sample position, test frequency, examination coverage, acceptance level, witness points and reporting format.
4. Align the supply condition
Confirm whether the price covers as-forged, heat-treated, proof-machined, rough-machined or finish-machined supply. Define surface condition, dimensional-report scope, marking, rust prevention, packing and dispatch documentation so competing offers cover the same work.
5. Review feasibility before commitment
Ask the manufacturer to record assumptions, exclusions and proposed deviations. A useful technical review explains what is accepted, what requires clarification and what must change before production. This review is more valuable than a generic capacity statement.
Common specification mistakes
- Specifying one hardness value without location or tolerance.
- Ignoring the transition between barrel and neck sections.
- Ordering from a sketch that lacks machining datum information.
- Comparing quotations without aligning testing and supply condition.
Another common error is copying an old purchase specification without confirming whether the service, material source, drawing revision or applicable standard has changed. Historical documents are useful references, but they still require current engineering approval.
Information to include in the RFQ
- Finished and forging drawings with revision numbers.
- Material grade, governing standard and permitted substitutions.
- Heat-treatment condition and target mechanical properties.
- Quantity, individual weight and anticipated repeat demand.
- Machining scope, allowances, datums and surface-finish requirements.
- Inspection methods, acceptance criteria, witness points and certificates.
- Required delivery date, packing, marking and dispatch destination.
How CS Heavy Forgings can review the requirement
For a capability review, send the controlled documents to info@csforge.in. The team can evaluate the enquiry against the relevant forged rolls information, published manufacturing range and available inspection route. Any quotation should be read with its stated assumptions and exclusions.
For requirements connected with Mandi Gobindgarh, Punjab or supply across India, location can support communication and logistics, but it does not replace technical qualification. The correct supplier is the one that can demonstrate a controlled route for the specific component.
Frequently asked questions
Is the title of this guide enough to create a purchase specification?
No. The guide identifies the questions to resolve. The approved drawing, material standard, quality plan and purchase order remain the controlling documents.
Can two quotations be compared only by price and delivery?
No. First align starting material, heat treatment, machining, inspection, certification, packing and exclusions. Otherwise the quoted scopes may be materially different.
Should a buyer accept an equivalent steel grade automatically?
No. Equivalence depends on the complete standard, chemistry, heat treatment, section size and required properties. Obtain written engineering approval before substitution.
When should inspection requirements be finalized?
Before production. Late inspection changes can affect stock size, sampling, heat treatment, machining and delivery.
What is the best first step for a custom enquiry?
Send the latest drawing, specification, quantity, supply condition, testing requirements and delivery need in one controlled RFQ package.
Discuss the component with CS Heavy Forgings
Email info@csforge.in or use the website quotation form. Include enough technical information for a meaningful feasibility review rather than a generic price response.